Home / Product / High-speed Guardrail Roll Forming Machine / W‑Beam Guardrail Roll Forming Machine
High-speed Guardrail Roll Forming Machine

W‑Beam Guardrail Roll Forming Machine

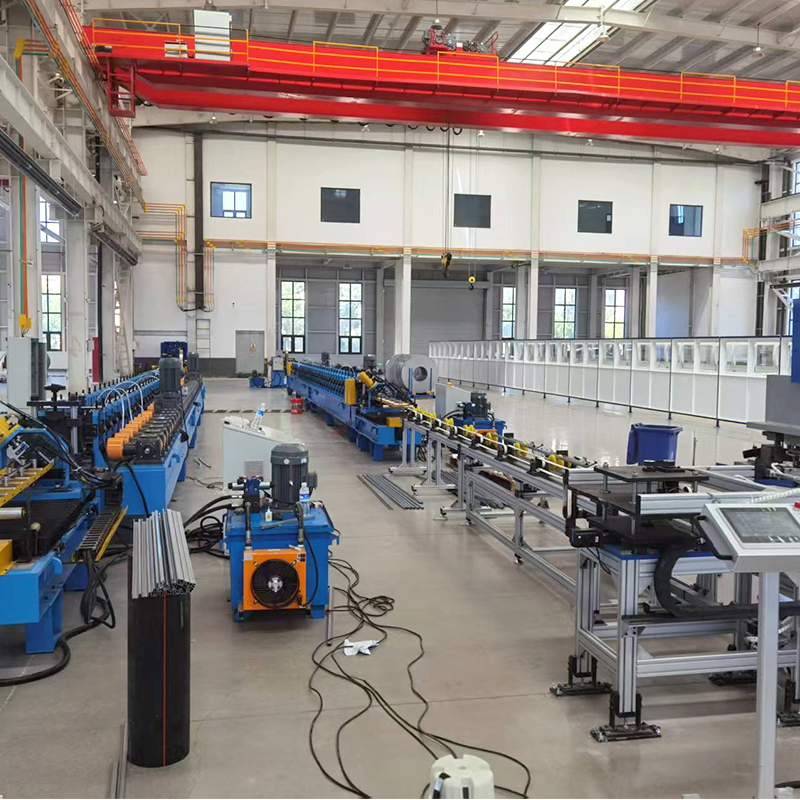
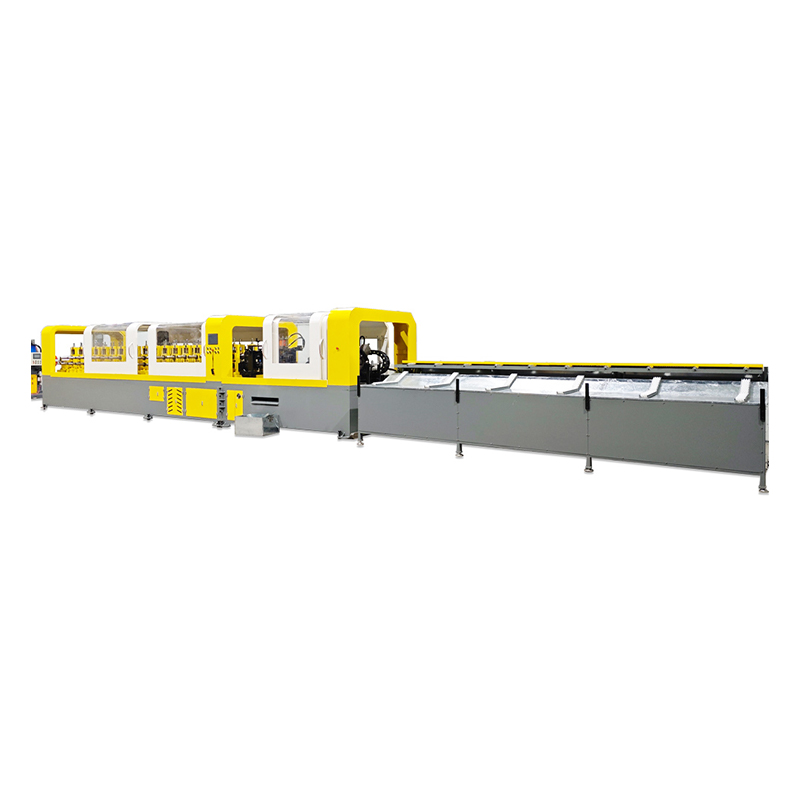
The W-Beam Guardrail Roll Forming Machine is an automated production line specifically designed for manufacturing two-wave corrugated beam guardrail panels for highways. The machine processes steel plates into standard corrugated guardrail panels through continuous roll forming, punching, and length cutting. The products are characterized by high strength and excellent impact resistance, and are widely used on highways, urban roads, bridges, and traffic safety protection projects.

W-Beam Guardrail Roll Forming Machine — Professional manufacturer, expert in heavy-gauge forming, precision intelligent manufacturing, high efficiency and stability.

Equipment Introduction

Parameter

Flowchart

Process Flow

Contact

Equipment Overview

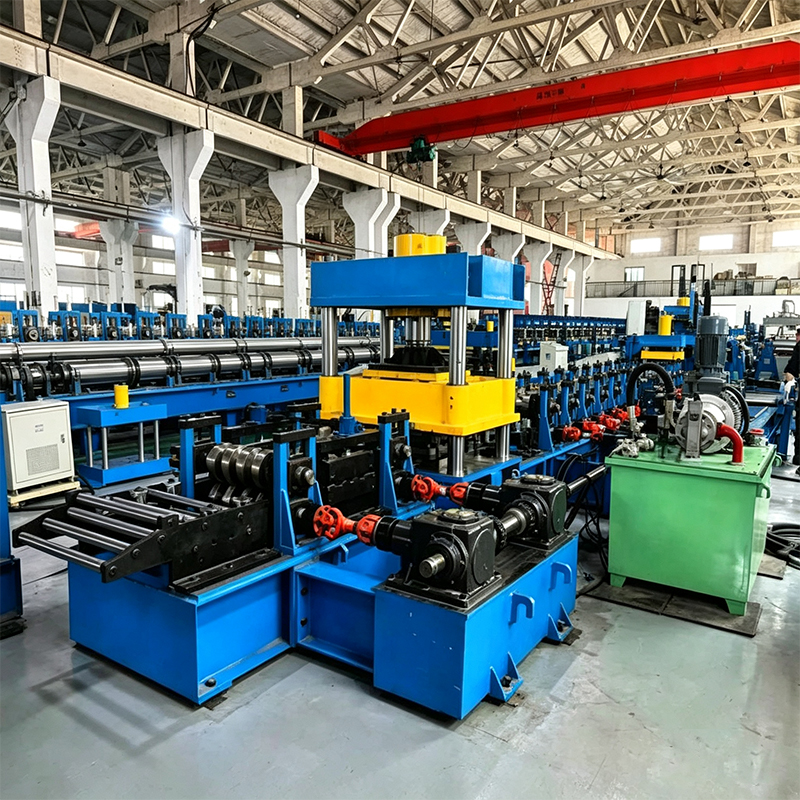
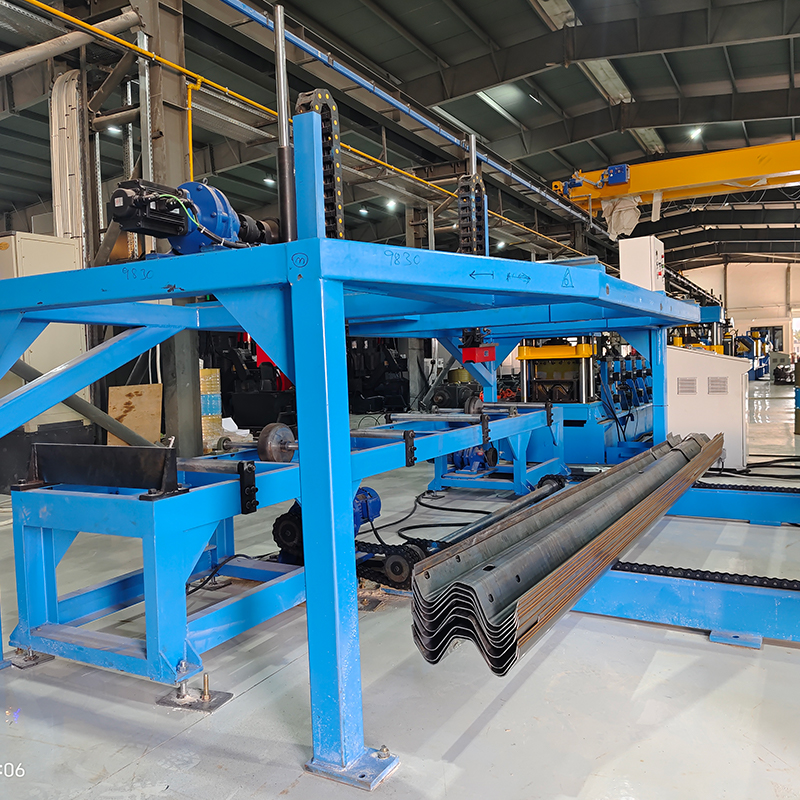
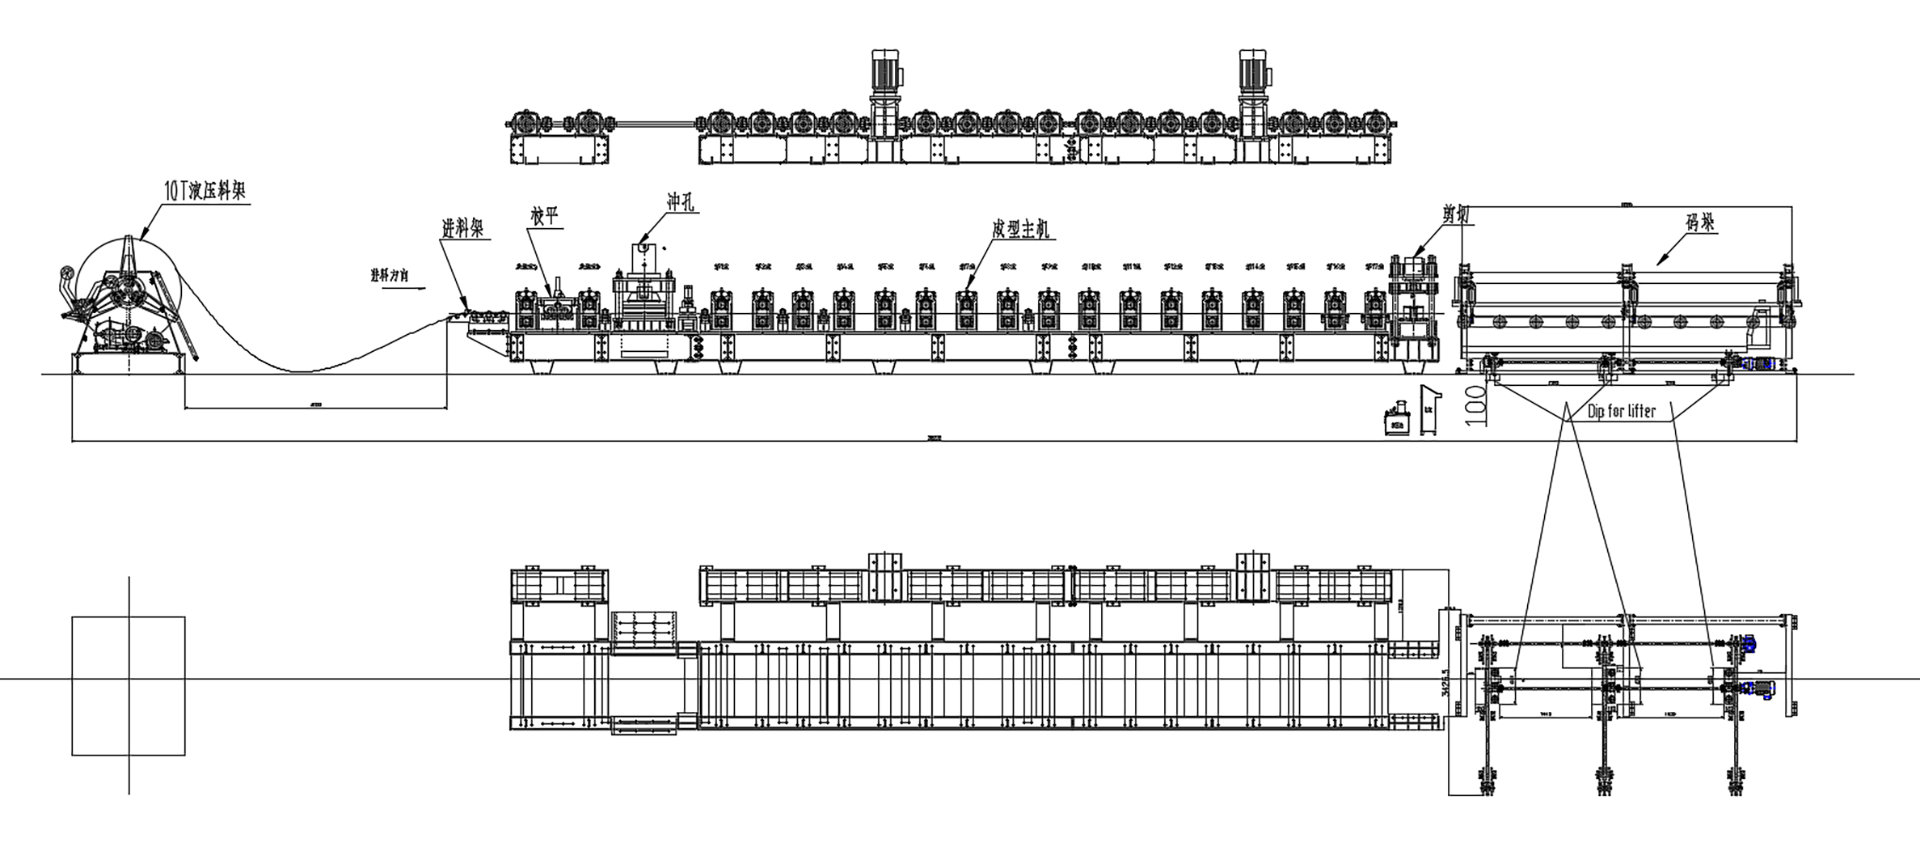
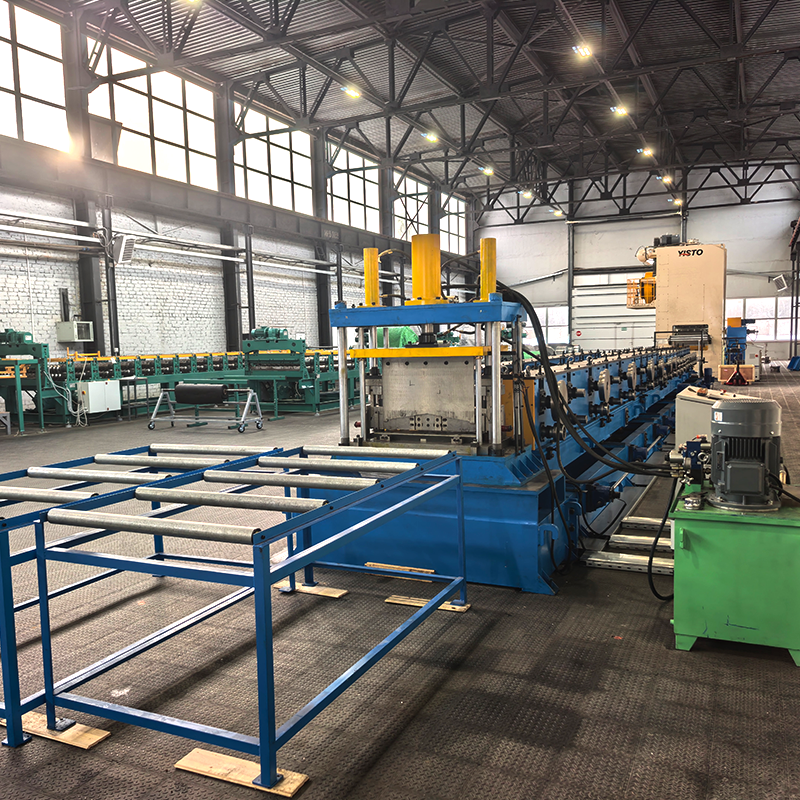
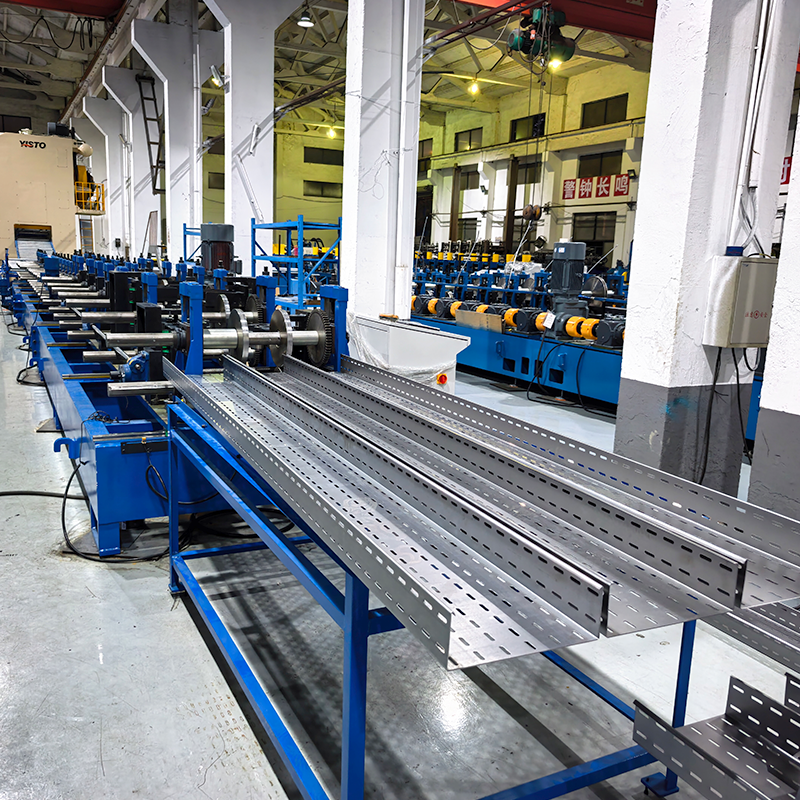
The W-Beam Guardrail Roll Forming Machine is specialized cold-roll forming equipment designed for the production of highway W-beam steel guardrail panels. W-beam steel guardrails—comprising both two-wave (W-beam) and three-wave (Three-beam) types—represent the most widely used form of guardrail today. The W-beam guardrail is a strip-shaped, energy-absorbing structure installed along the roadside or in the median strip; upon vehicle impact, it absorbs energy through structural deformation or by allowing the vehicle to ride up the rail, thereby mitigating injury to occupants. Utilizing a continuous cold-roll forming process, the machine integrates hydraulic uncoiling, guided feeding, pinch-leveling, hydraulic punching, roll forming, cut-to-length shearing, and palletized discharge into a single, streamlined operation, directly producing finished W-beam guardrail panels.

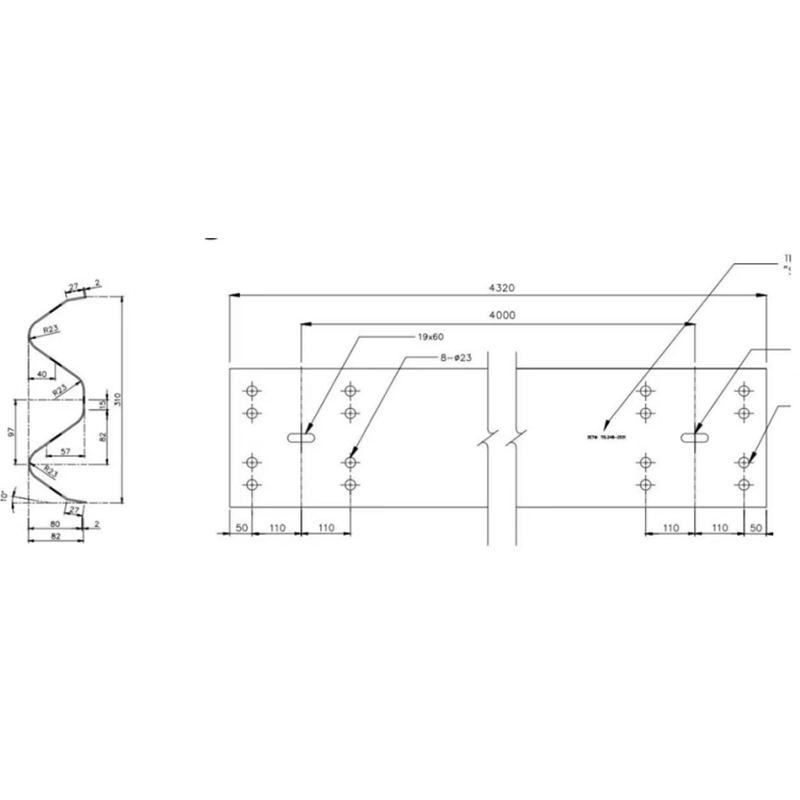
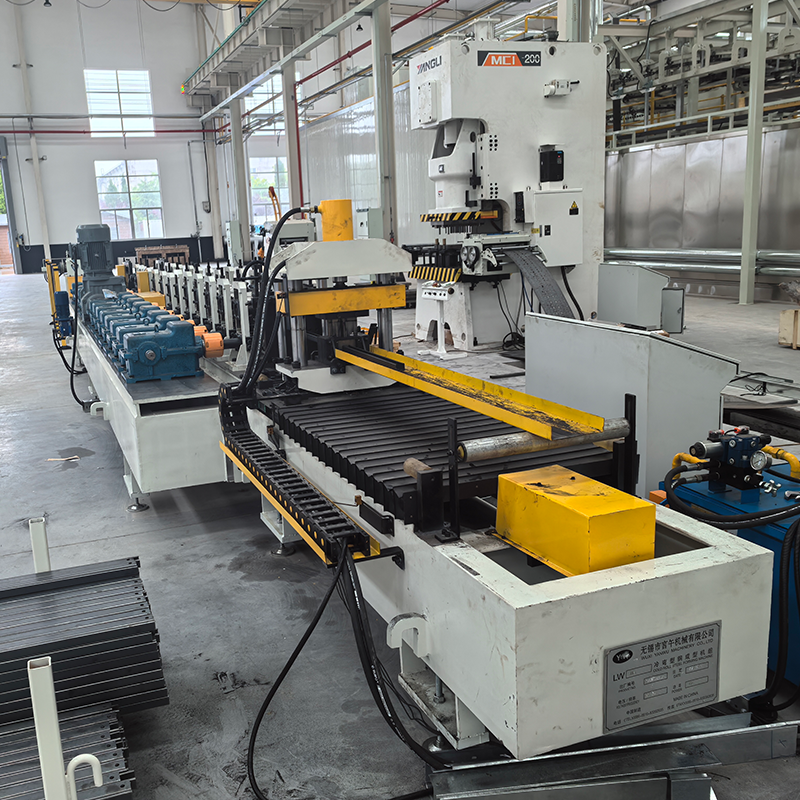
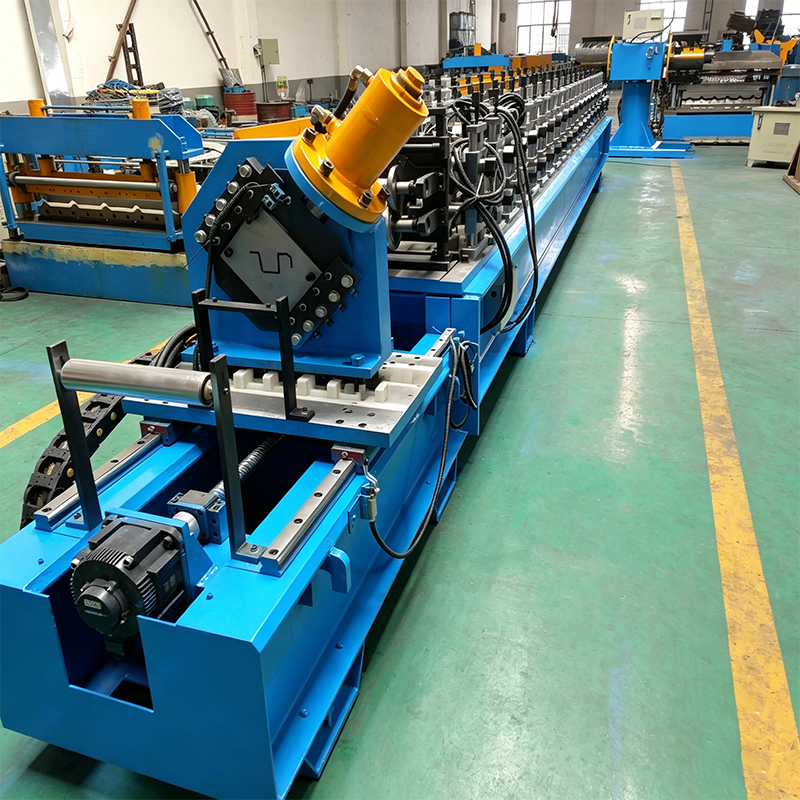
The entire line features fully automated PLC control and a touchscreen HMI, ensuring continuous, automated operation from uncoiling to finished product discharge. Key integrated units include a five-roller leveling system, a two-station four-column hydraulic punching unit (integrated within the main machine), and a 12-station main roll-forming unit. It employs a cast-iron arch-style gearbox transmission structure, offering high rigidity, precision, and durability. The equipment is compatible with various materials, such as Q235 and Q345 low-alloy high-strength steel, in thicknesses ranging from 2.0 mm to 3.0 mm, and is capable of producing standard W-beam guardrail panels (4320 × 310 × 85 mm). Requiring only 1–2 operators, this machine is essential equipment for highway guardrail manufacturers aiming to achieve large-scale, standardized, and intelligent production.

W-beam steel guardrails are classified into five crashworthiness levels—B, A, SB, SA, and SS—with the W-beam panel suitable for general road sections and moderate protection requirements. They are categorized by installation location (roadside or median) and by anti-corrosion coating type (single-layer or composite coating). Surface treatment options include hot-dip galvanizing or a dual-layer anti-corrosion system combining galvanizing with powder coating. The guardrail panels produced by this equipment strictly comply with the national standard GB/T 31439.1-2025, *Corrugated Steel Beam Guardrails – Part 1: Two-Wave Corrugated Steel Beam Guardrails*; this standard was issued on August 29, 2025, and officially implemented on March 1, 2026.


Core Advantages and Selling Points

(1) Cast-iron arch-style gearbox drive: High rigidity, high precision, and long service life

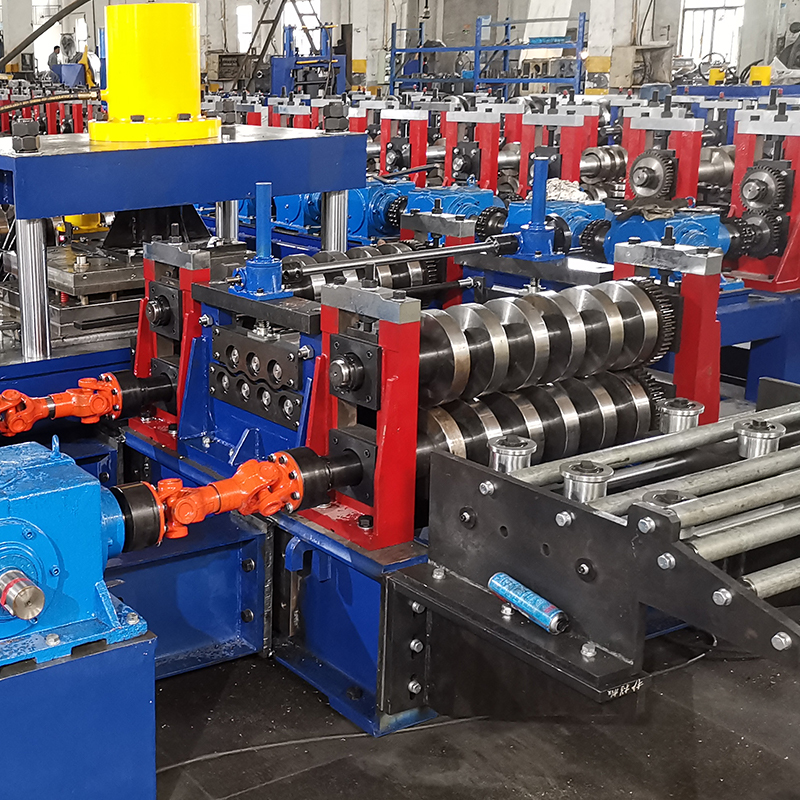
The forming machine utilizes a cast-iron arch-style gearbox drive structure, with each forming stand independently equipped with a gearbox; this is a key advantage distinguishing this equipment from conventional chain-driven models.

Compared to chain drives, gearbox drives offer significant advantages such as smooth operation, low noise, high precision, and extended service life. The cast-iron arch-style frames undergo tempering treatment to ensure high rigidity and excellent resistance to deformation, guaranteeing stable, high-intensity operation over long periods. The large-diameter forming shafts (Φ80mm) offer high load-bearing capacity and superior torsional resistance, specifically designed for the high-speed forming of 2.0–3.0mm thick plates.

(2) Five-roll leveling + dual-roll pinch feeding: Precise and reliable material pre-treatment

The leveling mechanism employs a configuration featuring dual-roll pinch feeding (at both entry and exit) and five-roll leveling, with leveling roll diameters of Φ90 mm. The pinch-feed rolls provide stable feeding power, while the five-roll precision leveling effectively eliminates internal stresses in 2.0–3.0mm thick plates, ensuring the steel strip enters the subsequent punching and forming stages in a flat, precise condition. The integrated design of pinch feeding and leveling lays a solid foundation for high-precision forming, effectively preventing defects caused by material unevenness.

(3) Two-station four-column hydraulic punching (integrated into the main unit): High force and high precision

The punching mechanism utilizes a four-column hydraulic structure (with the punching frame constructed from welded steel plate and tempered). Its two-station design allows punching to be completed within the main unit; this integration combines punching and forming into a single machine unit, eliminating intermediate transfer steps and resulting in higher positioning accuracy and a streamlined workflow. The four-column structure ensures high rigidity and guiding precision, while the hydraulic system delivers substantial force and cutting power, specifically designed for 2.0–3.0mm thick plates. The two-station setup enables the simultaneous punching of various hole types—such as connection bolt holes and splicing bolt holes—while the integration with the main unit minimizes hole-position deviation and enhances product consistency.

(4) 12-Stand Multi-Pass Forming for Consistent Corrugation

Utilizing a 12-stand, multi-pass progressive cold-roll forming process, the system optimizes mold design and forming parameters through precision algorithms to ensure product accuracy from the source. The 12-stand layout is scientifically designed to gradually bend 2.0–3.0mm thick plates into the standard corrugated profile. This multi-pass progressive forming effectively minimizes material stress concentration, ensuring consistent corrugation and stable cross-sectional dimensions. The forming line speed ranges from 0 to 15 m/min (excluding punching and cutting); based on a standard panel length of 4320mm, the system can produce 2–3 guardrail panels per minute, meeting high-volume production demands.

(5) High-Precision Fixed-Length Cutting (±1.0mm)

Length precision reaches ±1.0mm—far exceeding industry standards—effectively ensuring accuracy during guardrail installation and splicing. A stable product pass rate significantly reduces raw material waste and rework costs. The corrugated guardrail panels meet strict standards for straightness and twist, effectively preventing misalignment during installation.

(6) High-Power Drive System

The forming machine is equipped with a 22kW motor, providing ample power to ensure stable and efficient processing of 2.0–3.0mm thick plates across the 12 forming stands. Key electrical components are sourced from internationally renowned brands, ensuring low failure rates and a long service life.

(7) Quenched Cr12MoV Rollers for Durability and Precision

The roller set is made of Cr12MoV steel and undergoes quenching treatment (HRC 58–62), resulting in high hardness and excellent wear resistance. Cr12MoV is a premium cold-work die steel known for high hardness, superior wear resistance, and good hardenability. After quenching, it achieves a hardness of HRC 58–62, ensuring long mold life and stable precision, which guarantees consistent quality during long-term, high-volume production.

(8) Intelligent Control and User-Friendly Operation

Features fully automatic PLC control and a touchscreen HMI (Human-Machine Interface) to enable digital management of the entire process. Operators can configure parameters such as production speed and cut length via the interface with a single touch. The equipment offers both manual and automatic operating modes to suit various production scenarios. Multiple safety protection measures are implemented during standard operation to ensure operator safety. It is equipped with real-time monitoring and fault warning systems that automatically trigger alarms and display the cause of any malfunction. Novices can become fully independent after just 1–2 days of training, significantly lowering the required skill level for operators.


Technical Parameters

Item | Parameter
Applicable materials | Q235, Q345 low-alloy high-strength steel, etc.
Material thickness | 2.0–3.0 mm
Produced profile | Two-wave (W-beam)
Product specifications | 4320 × 310 × 85 mm (Standard two-wave panel)
Forming machine structure | Cast-iron arch-style frame with gearbox drive
Leveling mechanism | Front and rear dual-roller pinch feed + 5-roller leveling
Leveling roller diameter | Φ90 mm
Punching mechanism | Four-column hydraulic punching (welded steel punching frame, tempered)
Punching stations | 2 stations (punching performed within the main machine)
Shaft diameter | Φ80 mm
Main motor power | 22 kW
Forming line speed | 0–15 m/min (excluding punching and cutting)
Forming stages | 12 main roller stations
Cut-to-length accuracy | ±1.0 mm
Roller tooling | 1 set
Roller material | Cr12MoV, quenched (HRC 58–62)
Control system | Fully automatic PLC control
Operators | 1–2 persons


Production Process

Hydraulic Uncoiling → Guided Feeding → Pinching & Leveling → Hydraulic Punching → Roll Forming → Cut-to-Length → Discharge

Process Step | Description
Hydraulic Uncoiling | Hydraulic uncoiler supports the steel coil and ensures stable material feeding; maximum load capacity is customizable.
Guided Feeding | Automatic material guiding and alignment ensure the steel strip enters the leveling unit in the correct position.
Pinching & Leveling | Features front and rear pinch rollers and a 5-roller leveling system; precision leveling via Φ90mm shafts eliminates internal stress in 2.0–3.0mm thick plates.
Hydraulic Punching | 2-station, four-column hydraulic punching (integrated into the main machine) for punching connection and splicing bolt holes.
Roll Forming | 12-stand progressive cold roll forming gradually shapes the thick plate into a double-wave profile.
Cut-to-Length | Hydraulic cutting with a length accuracy of ±1.0mm; produces clean, smooth cut edges.
Discharge | Output of finished products; ensures orderly discharge.


Application Areas

W-beam guardrail panels produced by the high-speed 2-wave cold-roll forming machine are widely used in the following areas:

Expressways: Safety protection along the sides and central medians of expressways; W-beam steel guardrails are the most widely used safety facilities on expressways, with the 2-wave type suitable for sections requiring standard protection levels.

National and Provincial Trunk Highways: Safety protection for Class I and Class II highways; 2-wave guardrail panels are suitable for moderate protection requirements and offer an economical, practical solution.

Rural and Mountain Roads: County roads, township roads, and hazardous sections in mountainous areas; guardrail panels with thicknesses of 2.0–3.0 mm are economical and practical, meeting basic protection needs.

Bridges and Tunnels: Bridge transition sections and tunnel entrances/exits; used in conjunction with specialized bridge guardrails.

Municipal Roads and Urban Expressways: Urban elevated roads and expressways; W-beam guardrails are aesthetically pleasing, durable, and easy to maintain.

Industrial Parks and Factory Roads: Safety protection for internal roads within large industrial parks and logistics parks.

Tourist Attraction Roads: Winding mountain roads and cliff-side sections within scenic areas; W-beam guardrails provide reliable safety protection.

Airports and Ports: Roads surrounding airports and internal roads within port terminals.


Market Outlook

Driven by the continuous advancement of global infrastructure development, the highway guardrail market is experiencing steady growth. The global market for highway guardrail components is valued at approximately US$1.259 billion in 2025 and is projected to reach US$1.783 billion by 2032, reflecting a compound annual growth rate (CAGR) of 5.1%. China's roadside safety barrier construction market is estimated at US$1.92 billion in 2025 and is expected to grow to US$2.63 billion by 2031, with a CAGR of 5.43%. The domestic road guardrail market reached a scale of RMB 38.76 billion in 2025—a year-on-year increase of 12.4%—and is projected to surpass RMB 43 billion in 2026, maintaining a growth rate between 11% and 13%. W-beam guardrails account for 78% of the highway guardrail market share.

On August 29, 2025, the Standardization Administration of China (SAC) released the national standard GB/T 31439.1-2025, "Corrugated Steel Beam Guardrails – Part 1: Two-Wave Corrugated Steel Beam Guardrails," which is set to take effect on March 1, 2026. The implementation of this new national standard will further regulate the production and inspection requirements for W-beam guardrail panels, impose stricter demands on manufacturing equipment, and create broader market opportunities for high-quality guardrail panel forming equipment.

A nationwide transition from "two-wave" to "three-wave" guardrail panels is currently underway; this involves replacing the standard two-wave panels (featuring two curved sections) with three-wave panels, which are wider and offer superior impact resistance. As road safety standards rise and the new national standard is implemented, design and performance requirements for corrugated guardrail panels are becoming increasingly stringent, driving sustained demand for high-quality forming equipment. Corrugated steel beam guardrails are a classic cold-formed steel product; given the continued investment in transportation infrastructure and the ongoing elevation of road safety standards, the market demand for high-quality, high-precision corrugated guardrail panels is expected to keep growing.


Service & Support

Solution Design: Personalized equipment selection and production line layout based on customer product drawings, capacity requirements, and target markets.

Custom Manufacturing: Support for non-standard customization, with full control over the process from roll design to complete line manufacturing.

Installation & Commissioning: On-site installation, commissioning, and operator training provided by engineers to ensure rapid production startup.

After-Sales Support: Long-term technical consultation and spare parts supply; engineers hold valid visas and are available for on-site service worldwide at any time.

Continuous Optimization: Equipment modification and capacity upgrade services available to adapt to changing production needs.


Why Choose Us

Nearly 20 Years of Manufacturing Experience: Mature technology, refined processes, and reliable quality.

Thick-Plate Forming Expert: Covers thicknesses of 2.0–3.0mm; specifically designed for highway guardrail panels.

Rugged and Durable: Cast-iron arch-style gearbox drive, large Ø80 mm shaft diameter, and Cr12MoV quenched rollers (HRC 58–62).

Integrated Punching and Forming: Two-station, four-column hydraulic punching performed within the main unit; precise positioning and a compact workflow.

High-Precision Manufacturing: Length accuracy of ±1.0mm and a stable product pass rate.

Efficient Production: Line speed of 15m/min; daily capacity meets high-volume supply demands.

Intelligent Control: Fully automatic PLC system with touchscreen operation; the entire line can be operated by just 1–2 people.

Direct Manufacturer: No middlemen; excellent cost-performance ratio.

Global Service Network: Engineers hold all necessary visas; rapid response capabilities.
Item Specification
Forming machine structure Cast-iron arch-style frame with gearbox drive
Leveling mechanism structure Front and rear dual-roller pinch feed; five-roller leveling
Leveling shaft diameter Φ90mm
Punching mechanism structure Four-column hydraulic punching (punching frame made of welded steel plate with tempering treatment)
Punching stations 2 stations
Shaft diameter Φ80mm
Forming machine motor power 22kW
Forming machine line speed 0–15 m/min (excluding punching and cutting time)
Forming stages 12 main roller stations
Rolling thickness 2.0–3.0mm
Length tolerance ±1.0mm
Roller tooling 1 set
Roller material Cr12MoV, quenched (HRC 58–62)

LWvy1

Hydraulic uncoiling — Guiding & feeding — Pinching & leveling — Hydraulic punching — Roll forming — Cut-to-length — Discharge onto support table

We can provide you with a satisfactory plan!

What's your name?

What's your email address?

What's your telephone?

Your message

SEND
About
Wuxi Yanwu Xinhui Technology Co., Ltd.

Established in 2012, Wuxi Yanwu Machinery Co., Ltd., is a professional manufacturer specializing in the R&D, design, manufacturing, and servicing of cold roll forming equipment. The company is dedicated to providing global customers with integrated solutions for automated cold roll forming production lines.

Our main products include cable tray forming machines, racking forming machines, C/Z purlin machines, solar mounting bracket forming machines, floor deck machines, door frame machines, automotive profile equipment, and cut-to-length/slitting lines.

These products are widely used in the construction, electrical power, logistics and warehousing, automotive manufacturing, new energy, and infrastructure sectors.

Certificate Of Honor
News
  • The new generation of slot-type cable tray cold bending forming machine has been officially launched. It is targeted at cable tray manufacturing enterprises and focuses on the profile production requirements of power infrastructure, data centers, and new energy supporting projects. With an integrated continuous cold bending process, it addresses the industry pain points of traditional split bending processes, such as poor accuracy, low efficiency, and high labor costs. It provides cable tray manufacturers with automated and highly stable profile production equipment solutions. With the continuous construction of new power systems, data centers, factory and municipal distribution projects, slot-type cable trays, as protective support components for cables, have higher requirements for profile size consistency, forming strength, and delivery cycle. The traditional processing mode often involves individual bending of plates and secondary punching, with multiple process flows, which are prone to bending deviations, hole misalignment, and incomplete jointing, resulting in high material loss and high dependence on skilled workers. This slot-type cable tray cold bending machine integrates opening, leveling, online punching, continuous roller pressing cold bending, servo fixed-length cutting, and material stacking. After the galvanized steel strip is sent to the production line, it is formed into a complete slot-type cable tray in one step, without the need for secondary processing. The equipment uses multiple precision rolling rollers for progressive cold bending forming, with a forming size error controlled within ±0.5mm, good slot body straightness, regular bending edges, strong finished product rigidity, and effectively guarantees the later cable tray jointing and installation accuracy. It is equipped with a PLC touch control intelligent system, allowing parameters to be set quickly, and it can quickly switch between various cable tray specifications, suitable for different width and height slot-type cable tray production. It is multi-purpose in one machine. The production line operates stably, forms quickly, significantly reduces the number of workers, reduces material loss, and improves production capacity. The equipment is compatible with various raw materials such as galvanized plates and color steel plates, and the produced slot-type cable trays are widely used in data centers, factory distribution, rail transit, photovoltaic and wind power, building construction, etc., meeting the requirements for the protection of strong and weak wire cables. The equipment adopts a modular structure design, is convenient for maintenance, supports customized functional upgrades, and can be connected to the existing automation production lines. Based on mature equipment research and manufacturing capabilities, it can provide customers with equipment debugging, technical training, and integrated after-sales operation and maintenance services, helping cable tray manufacturing enterprises achieve automation upgrades, reduce costs, increase efficiency, and empower the high-quality development of domestic and foreign power infrastructure supporting industries.
    READ MORE
  • Product Positioning and Core FunctionThe L-edge angle steel profile machine is a cold bending forming equipment specifically designed for manufacturing L-shaped cross-section steel profiles. The L-shaped profiles, as an important component of the steel profile system, are mainly used for connecting the ceiling and walls and reinforcing the corners of partition walls. In practical applications, this product can effectively solve problems such as warping of the edges and corners of the sheet material and unsightly gaps, thereby enhancing the overall decorative effect. Steel profiles are classified by cross-sectional form into various specifications such as V-type, C-type, T-type, L-type, and U-type. Among them, the L-type profiles, due to their unique right-angle structure, play an irreplaceable role in detailed construction processes such as edge finishing and corner sealing. Technical Features and Performance AdvantagesThe modern L-edge angle steel profile machine adopts the cold bending forming process. The galvanized steel strip is continuously bent and deformed through a group of gradually changing profile surfaces during the process at room temperature, ultimately forming an accurate L-shaped cross-section. This process route has significant advantages such as high material utilization rate, fast production efficiency, and good product consistency. In terms of automation control, the advanced L-type profile production line has achieved full-process automation operations. A typical production line configuration includes: an automatic two-in-one unwinding and leveling machine, a fully automatic servo tracking rolling system, high-precision and high-speed forming equipment, a fully automatic servo tracking shearing system, and core modules such as the support frame. Through the computer control system for tracking rolling and shearing, the equipment can simultaneously complete punching and cutting operations during the forming process, effectively replacing the traditional post-forming punching process, which saves labor and ensures product consistency. In terms of forming accuracy, the rollers made of high-strength mold steel such as Cr12MoV, after vacuum heat treatment, can reach a hardness of HRC58-62, ensuring long-term stable operation. Combined with the servo-driven feeding system, the feeding accuracy can be controlled within ±0.5mm, meeting the strict requirements of architectural decoration for the size accuracy of the profiles. Trend of Intelligent UpgradeCurrently, the L-edge angle steel profile machine is accelerating its evolution towards intelligence and flexibility. The PLC control system is equipped with a user-friendly touch screen interface, supporting multi-language operation and formula storage functions. Operators can quickly call up the production parameters of different specifications of products to achieve rapid model change. It is worth noting that the integration of laser cutting technology with the profile machine is becoming a new industry trend. Compared with traditional mechanical shearing, laser cutting has advantages such as smooth and hairless cutting edges, no contact with molds, and low noise. The cutting edge width can be controlled within 0.1- 0.3 mm. This technological breakthrough not only improves product accuracy but also enables economic small-batch and multi-variety customized production, providing a new solution for the processing of irregular components in prefabricated buildings. Market Prospects and Industry OpportunitiesFrom the investment dynamics of the steel profile equipment industry, the market for steel profile equipment remains active. For example, Guangdong Quan Tan Jing Gong Technology Co., Ltd. has a new project with a total investment of 150 million yuan, mainly engaged in the production of fully automatic universal steel profile machine production lines and conventional steel profile machines. After the project is completed, it is expected to produce 300 conventional steel profile machines annually. This investment scale reflects the continuous demand for steel profile equipment in the market. Industry analysis indicates that with the deepening of the concepts of prefabricated buildings and green construction, steel profiles, as a lightweight, high-strength, fire-resistant, and easy-to-install new type of building material, their application fields will continue to expand. From hotels, airports, shopping malls to office buildings and old building renovations, the steel profile system is playing an increasingly important role in various building scenarios. For the L-edge angle steel profile machine, the continuous expansion of the downstream application market will directly drive the growth of equipment demand. Advanced equipment with high precision, high efficiency, and intelligence will occupy a competitive advantage in this round of industrial upgrading.
    READ MORE
  • Technical upgrades lead industry development.The modern cold bending forming machine for automotive profiles has undergone a comprehensive upgrade from traditional hydraulic drive to servo drive technology. The servo motor-driven forming equipment not only improves positioning accuracy but also significantly reduces energy consumption and noise levels, with maintenance costs dropping sharply. In terms of forming accuracy, the axial repeat positioning accuracy of advanced equipment can reach -0.01 mm, and the upper wheel positioning accuracy reaches 0.02mm, which can meet the strict dimensional tolerance requirements of automotive structural components. The half-diameter bending capability is a significant technological breakthrough in current automotive profile cold bending forming machines. Through the four-axis positioning system and ball screw closed-loop variable frequency motor control system, the equipment can achieve one-time forming of irregular shapes such as egg-shaped and elliptical, minimizing deformation during the forming process to the greatest extent. This technological breakthrough makes it possible to achieve efficient production of complex structural components such as car window frames and body reinforcement beams. Intelligentization and automation are deeply integrated.Against the background of Industry 4.0, automotive profile cold bending forming machines are accelerating their evolution towards intelligence. The PLC control system is equipped with a user-friendly touch screen interface, supports multi-language operation, can store multiple product formulas, and enables rapid switching of different specifications of profiles. The intelligent parameter storage system significantly reduces the changeover time, and some advanced equipment can complete the mold change in 30 minutes, with an efficiency increase of 70% compared to traditional equipment. Full-process automation operations have become the industry standard. From feeding, guiding, and forming to welding, cutting, and packaging, the entire production line can operate without human intervention, with only 1-2 people on duty per production line. The integration of the automatic stacking system further reduces manual intervention, ensuring the neat stacking and efficient turnover of finished profile products. Continuous breakthroughs in lightweight material processing capabilitiesFacing the increasing demand for high-strength steel and aluminum alloy materials in the automotive industry, the technical adaptability of cold bending forming equipment is constantly improving. Modern equipment can handle materials such as strengthened steel and galvanized steel with thickness ranges of 0.3-5.0mm. The rollers use Cr12MoV mold steel after vacuum heat treatment, with a hardness of HRC58-62, ensuring no cracking during high-strength steel forming. To address the industry pain point of high-strength steel forming prone to rebound and cracking, equipment manufacturers have optimized the roller curve design and adopted multi-pass progressive roller pressing technology to effectively solve this technical problem. The section size tolerance can be stably controlled within ±0.2mm, the hole position accuracy is fine to ±0.1mm, and the product qualification rate can reach over 99.5%. The market prospect is broad.According to industry research, the cold bending forming machine market is experiencing a rapid growth period. In the automotive manufacturing field, with the explosive growth of the new energy vehicle industry, the production demand for core structural components such as battery trays and body reinforcement beams has significantly increased. The widespread application of lightweight materials and the increase in complex pipe component structures continue to drive the demand for advanced cold bending forming equipment. Industry insiders point out that in the future, cold bending forming technology will evolve towards multi-axis linkage and flexible manufacturing. The implementation of artificial intelligence and machine vision technologies will give equipment the ability to perform online quality inspection, and digital twin technology will be applied to forming process simulation, further reducing trial-and-error costs and accelerating new product development speed. Equipment manufacturers with the ability to provide customized solutions will gain a competitive advantage in this round of industrial upgrading.
    READ MORE
High-speed Guardrail Roll Forming Machine Industry knowledge