I. Equipment Introduction
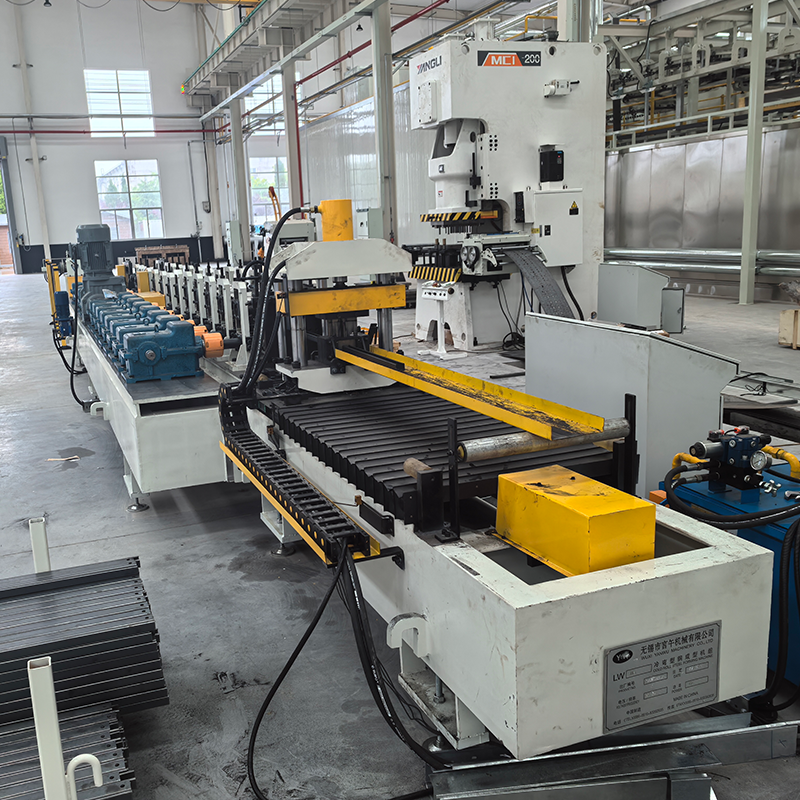
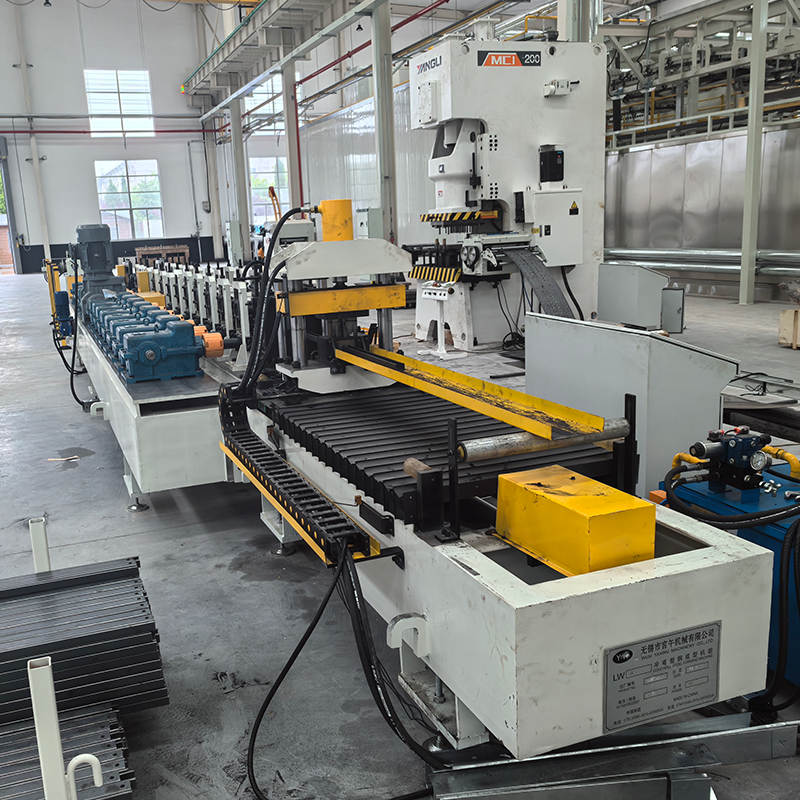
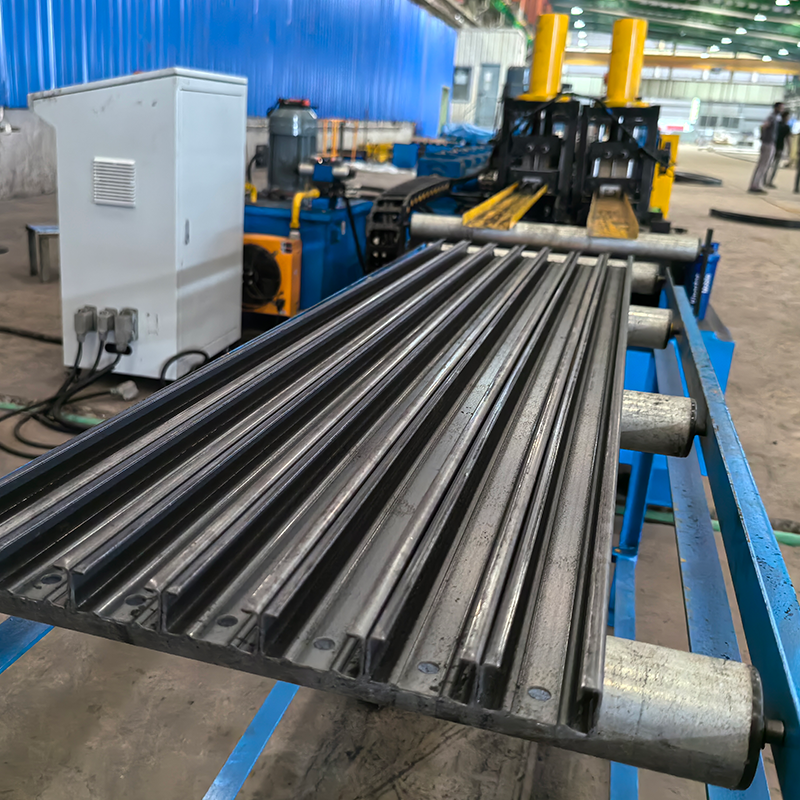
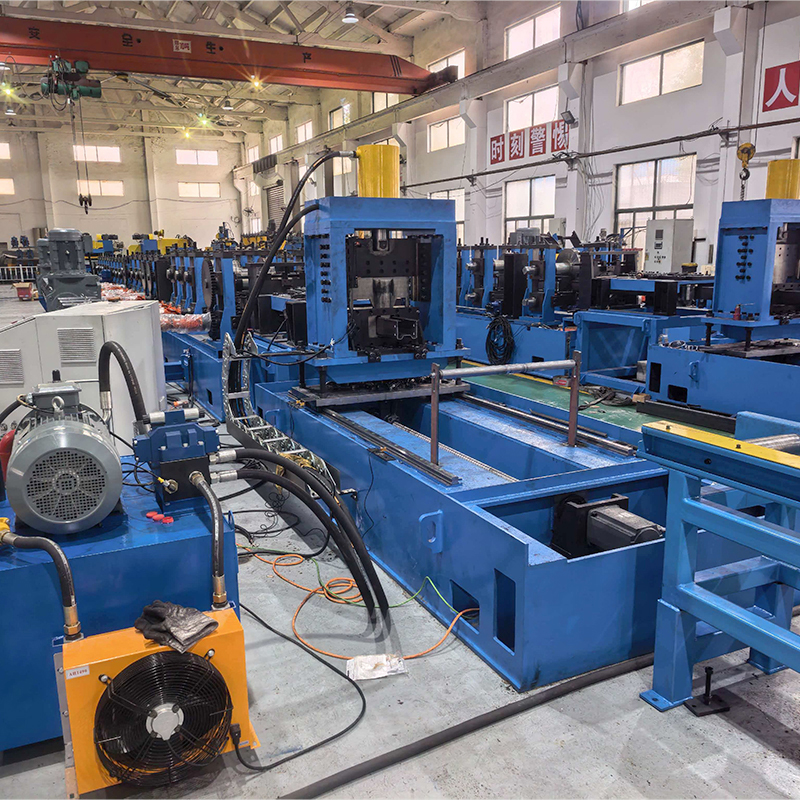
The diagonal brace roll forming machine is specialized equipment designed for the production of diagonal braces used in storage racking systems. Diagonal braces are critical structural reinforcement components; as inclined members within the support frame, they primarily bear axial loads. By providing diagonal reinforcement, they create a stable triangular structure between the uprights and beams, thereby significantly enhancing the rack's overall stability, torsional rigidity, and resistance to overturning.
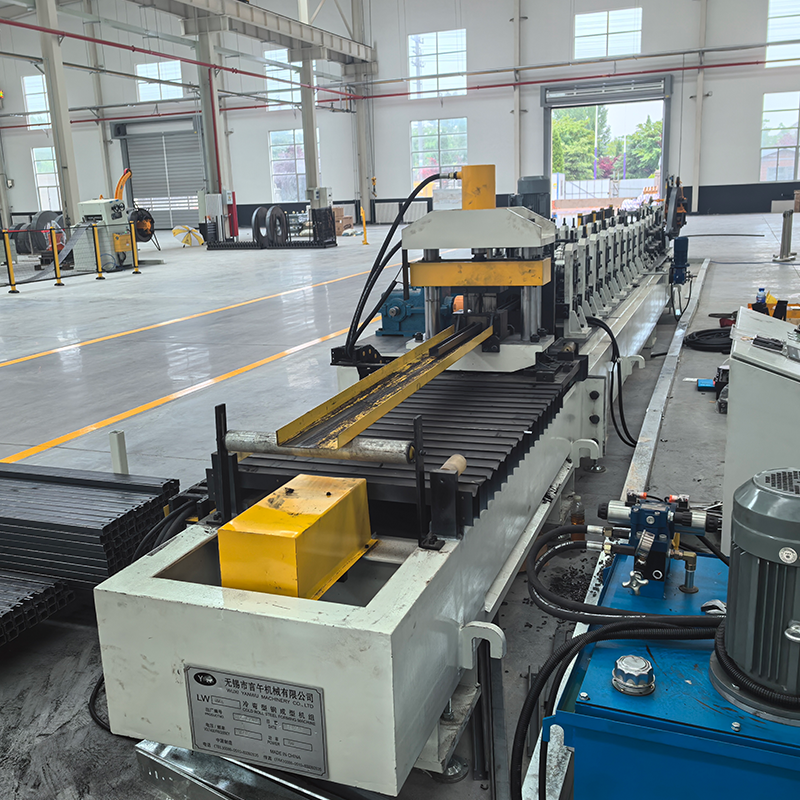
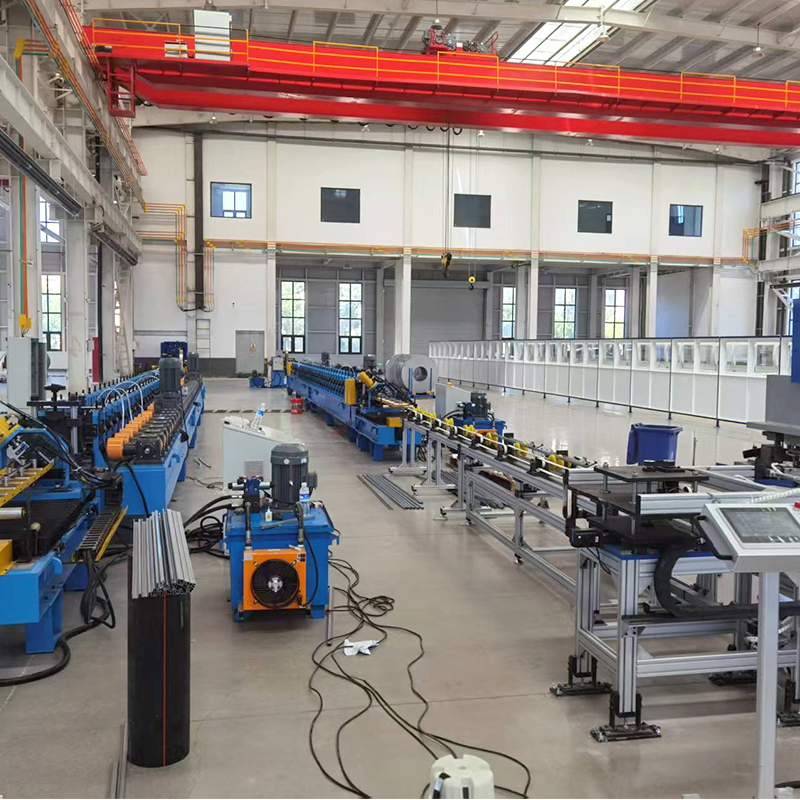
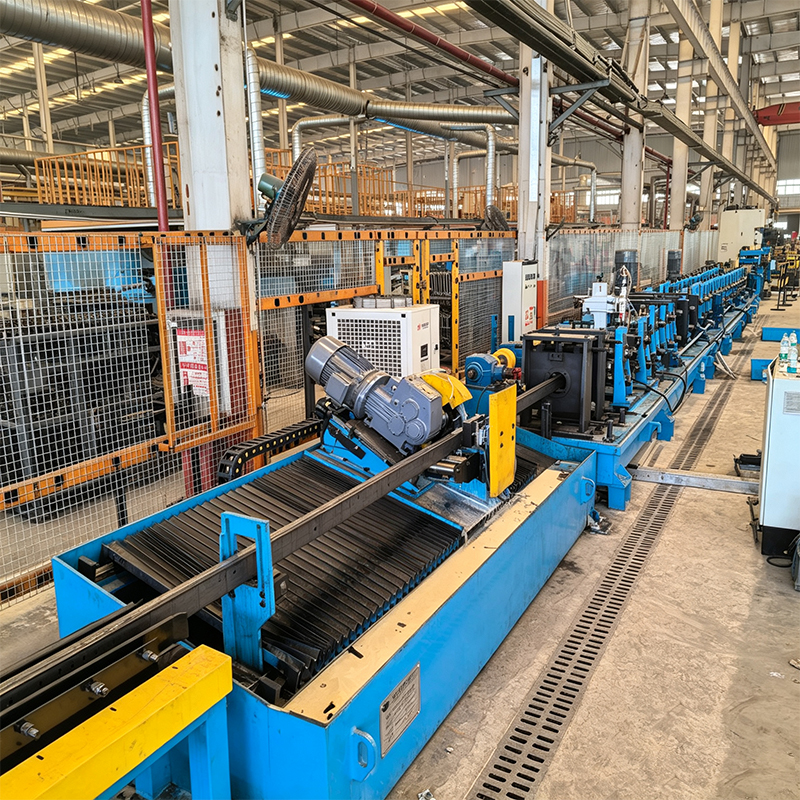
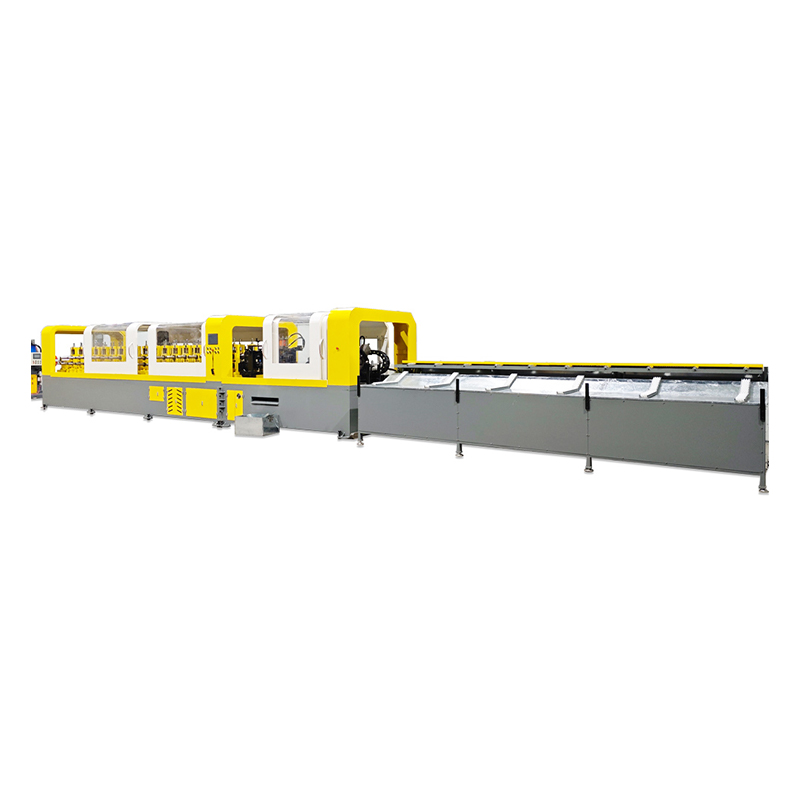
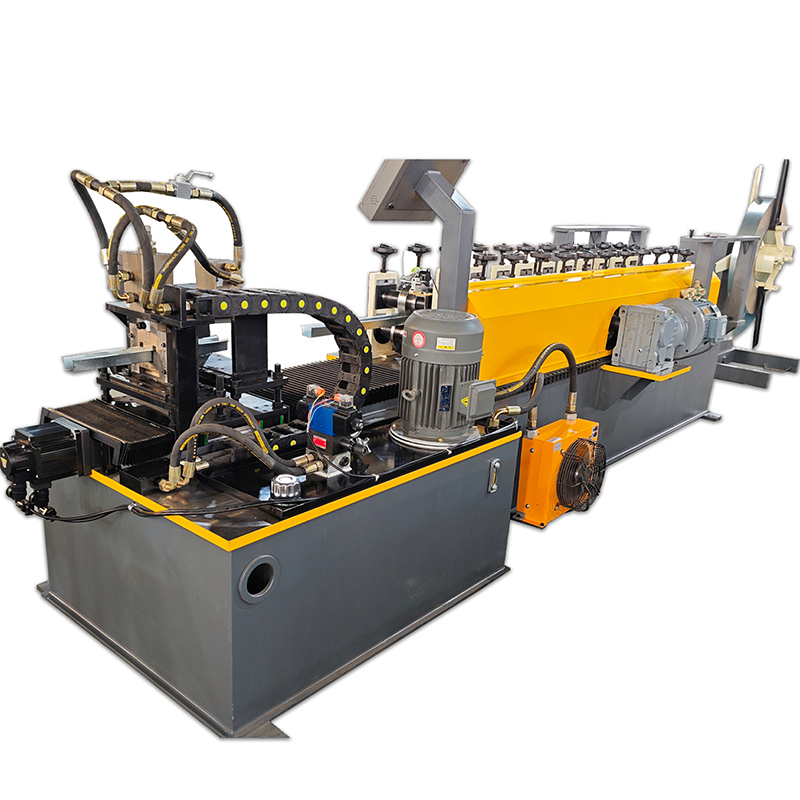
Utilizing a continuous cold-roll forming process, the machine transforms steel coil stock into finished diagonal braces through an integrated sequence of operations: uncoiling, leveling, feeding, punching, roll forming, and cut-to-length shearing. By combining punching, forming, and cutting into a single production line, the system enables a "one-person, one-machine" operation model with "one-touch" production capabilities.
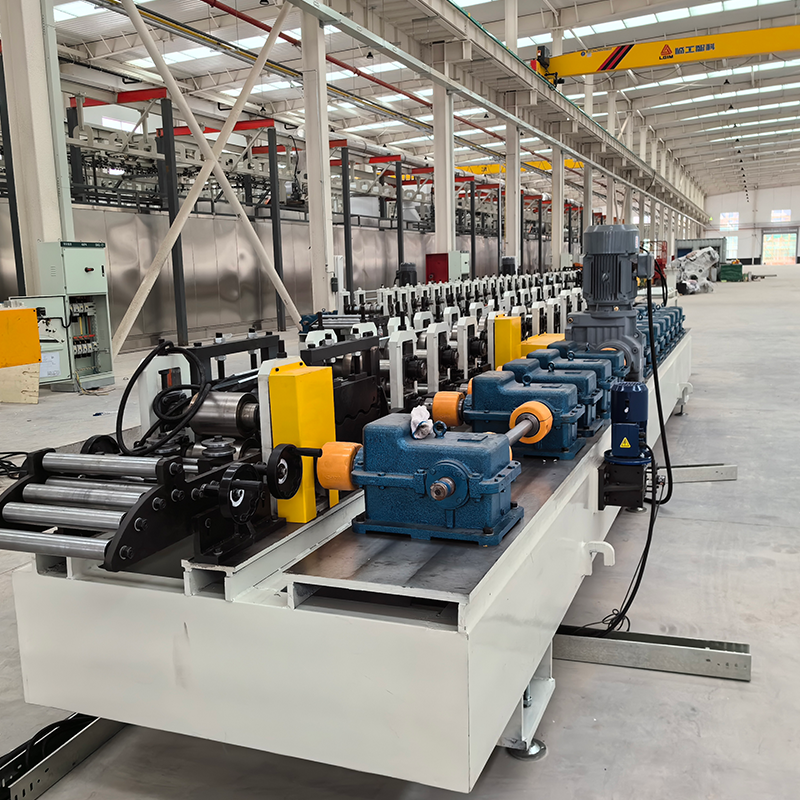
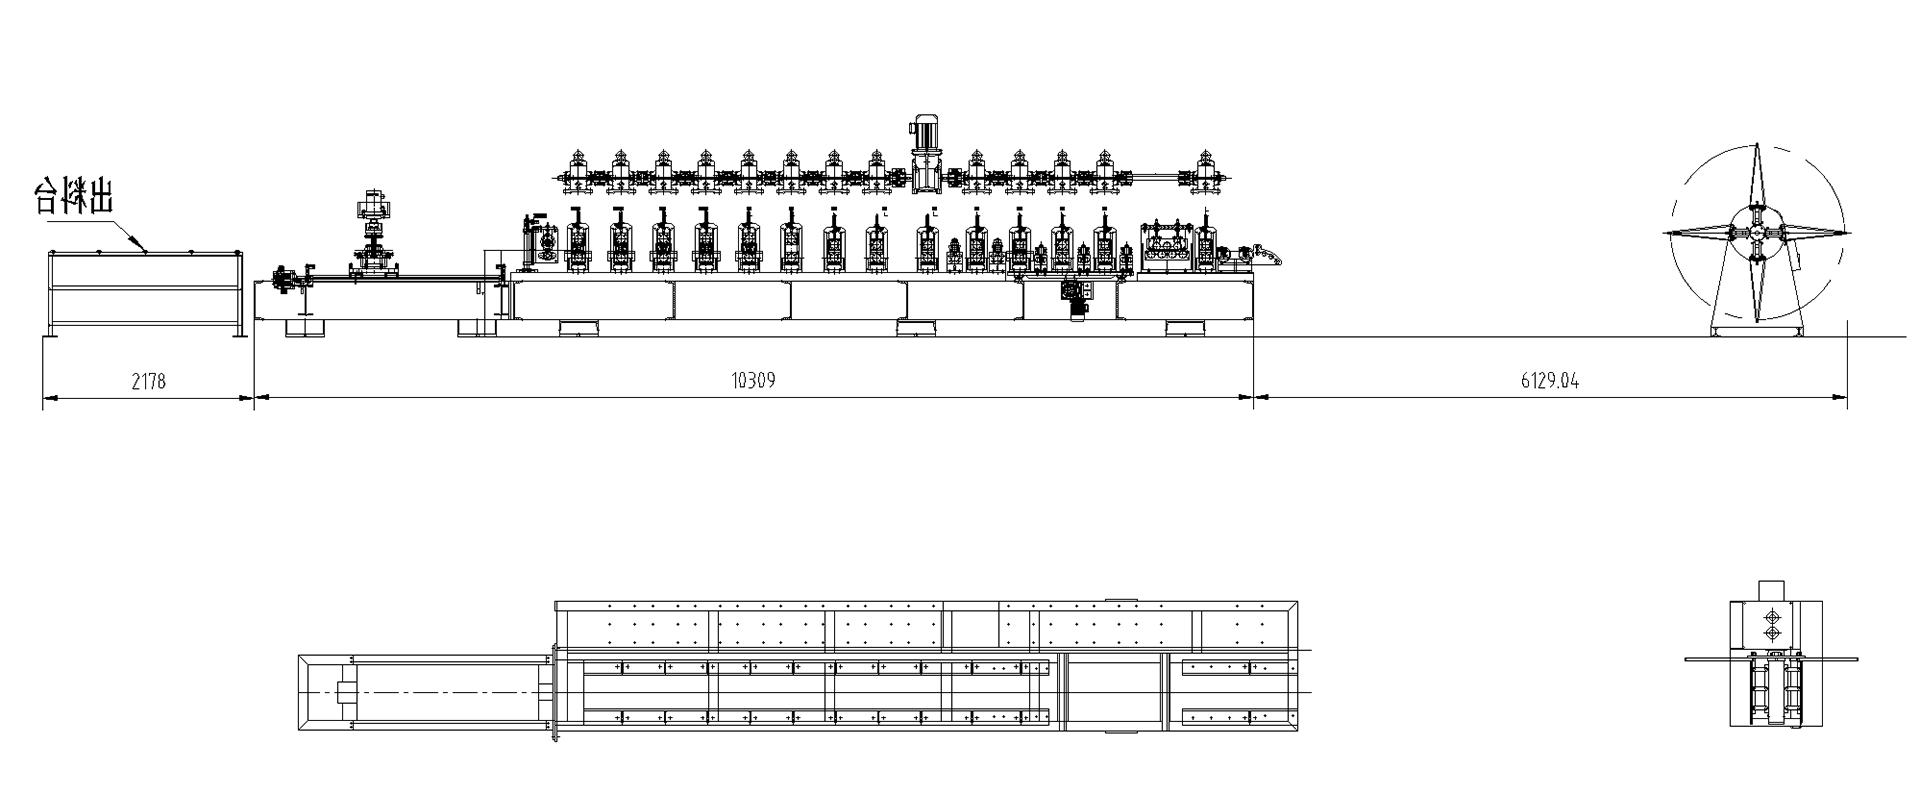
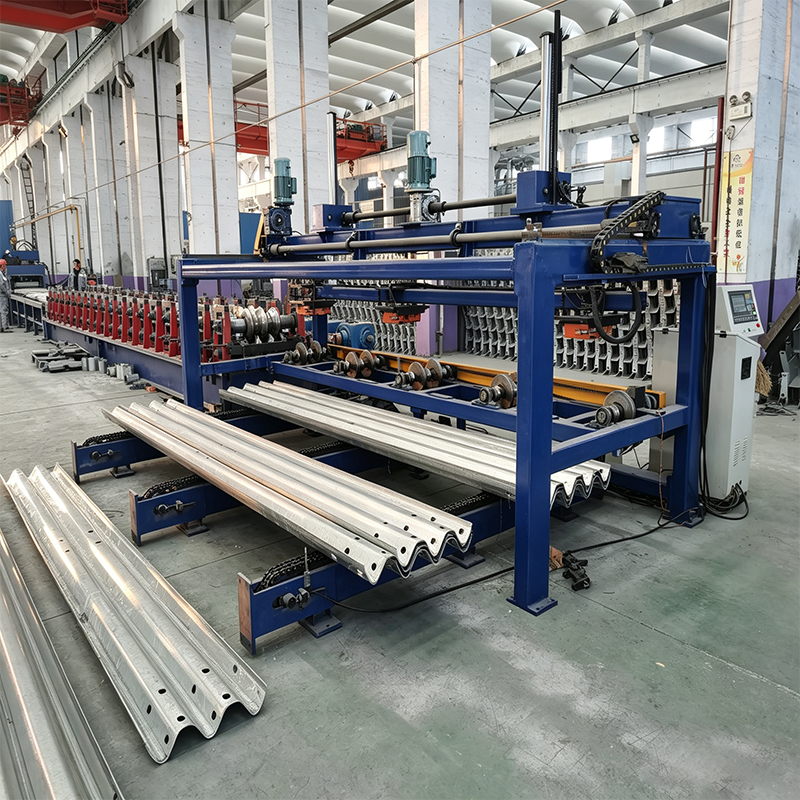
The equipment comprises several key components: an automatic uncoiler, a guide frame, a leveling/feeding unit, a continuous punching unit, a forming unit, a cut-to-length unit, a run-out table, and an electrical control cabinet. The entire line features fully automatic PLC control and a touchscreen HMI (Human-Machine Interface), ensuring a high degree of automation, ease of operation, and superior production efficiency.
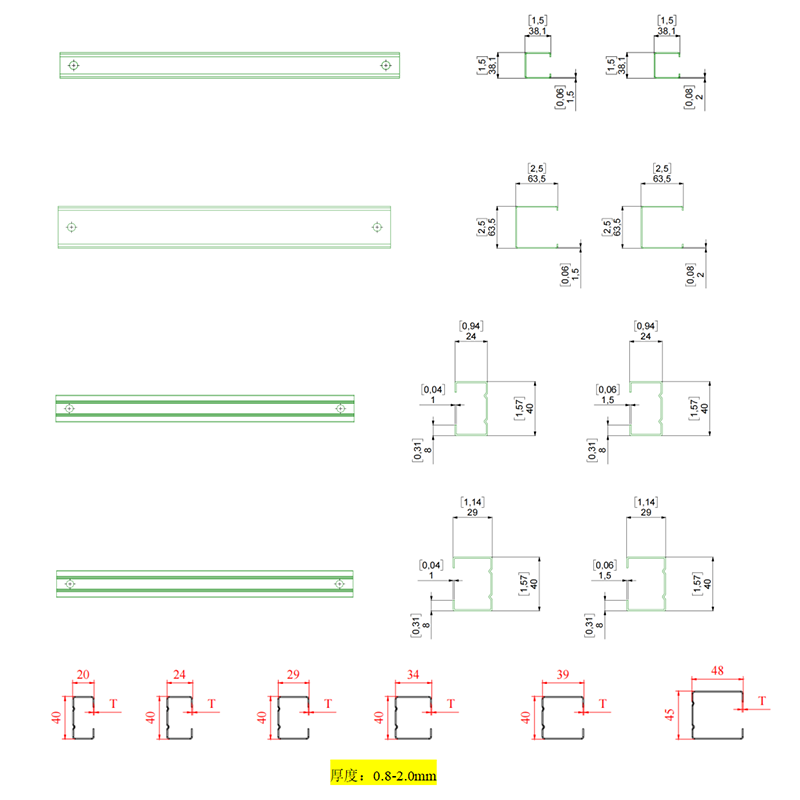
The machine is compatible with various metal sheet materials—such as cold-rolled steel, galvanized steel, and high-strength steel—and can produce diagonal braces with diverse cross-sectional profiles, including C-shapes, U-shapes, circular, and rectangular sections. It accommodates material thicknesses ranging from 0.6 mm to 2.5 mm (customizable), with widths tailored to specific customer requirements. The length of the diagonal braces can be flexibly adjusted to match rack heights, making them suitable for various racking systems, including selective pallet racks, drive-in racks, and mezzanine racking.
II. Core Advantages and Selling Points
1. Structural Reinforcement: The Key to Rack Safety
Diagonal bracing rods are the most critical safety reinforcement components in a racking system. By diagonally connecting uprights and beams to form a stable triangular support structure, they effectively withstand external forces such as seismic activity, forklift collisions, and uneven load distribution. Capable of withstanding lateral impact forces of several tons, they ensure the rack remains stable under extreme conditions, thereby preventing collapses. Diagonal bracing primarily reinforces the rack structure, creating a more integrated load-bearing framework and ensuring overall structural stability. 2. Versatile functionality; compatible with various diagonal bracing layouts
Produces X-type bracing: Suitable for racks with large spans and heights; evenly distributes loads in two directions, enhancing torsional and overturning resistance.
Produces K-type bracing: Suitable for space-constrained environments or scenarios requiring easy installation; effectively improves lateral rack stability.
Produces single diagonal bracing: Features a simple structure; suitable for areas with limited space and relatively lower load-bearing requirements.
Produces double diagonal bracing: Forms a stable triangular structure using two symmetrically arranged diagonal members; commonly used for heavy-duty and high-rise racking systems.
3. Diverse cross-sections to meet varying load-bearing needs
The equipment produces diagonal bracing members in various cross-sectional shapes:
C-section bracing: Reduces self-weight while maintaining strength, enabling lightweight design and lowering material costs.
Rectangular tube bracing: Offers high flexural and torsional rigidity; adapts well to complex stress conditions; suitable for components subject to significant bending and torsional loads.
Round tube bracing: Features isotropic mechanical properties and low wind resistance; suitable for wind-load-sensitive applications or space-constrained areas.
Square bracing: Performs exceptionally well under high axial forces and bending moments, providing stable support.
4. High-efficiency production with industry-leading output
Forming speeds range from 2 to 15 meters per minute.
Fully automated, continuous production line requiring only one operator.
Multiple processes integrated into a single machine, significantly shortening production cycles.
Ideal for high-volume, continuous production requirements.
5. High-precision forming for superior quality
Utilizes a multi-stage progressive cold-roll forming process, ensuring high dimensional accuracy and consistency.
Roll stands feature a robust arch-frame structure for high rigidity.
Roll shafts are made of high-quality steel and precision-machined to ensure assembly accuracy.
Rollers are made of GCr15 or Cr12MoV steel, heat-treated, precision-turned, and hard-chrome plated for high hardness and wear resistance.
Roll shafts are made of 40Cr steel and undergo quenching and tempering treatment.
6. Smart Control, Easy Operation
Fully automated PLC control with a touchscreen HMI; parameter settings are intuitive and convenient.
Utilizes a high-precision PLC control system (Delta/Schneider) for efficient and stable operation.
Touchscreen operation: simply input production data, and the system automatically fulfills production requirements.
Features automatic fault diagnosis and alarms for quick troubleshooting and maintenance.
Significantly reduces the skill level required for operators.
7. Rugged, Durable, Stable, and Reliable
The machine bed is a welded steel structure, tempered to relieve internal stress and prevent deformation.
The forming frame is made of cast iron and tempered to ensure high strength and a long service life.
The cutting blade is made of heat-treated Cr12MoV steel, offering a cutting lifespan of over 1 million cycles.
Driven by a motor with a gear-and-chain transmission system for smooth, reliable operation.
Key electrical components are sourced from renowned brands such as Delta and Schneider.
8. Material Savings and Cost Reduction
Employs a precision cold-roll forming process, ensuring high material utilization. The equipment can produce diagonal braces and tie rods in various lengths and sizes to meet different shelving height requirements, thereby minimizing material waste.
III. Technical Parameters
Item Parameter
Applicable materials: Cold-rolled sheet, galvanized sheet, high-strength steel
Material thickness: 0.6–2.5 mm (customizable)
Material width: Customized according to client requirements
Forming stations: 12–18 stations
Forming speed 2–15 m/min (customizable)
Main motor power: 7.5–30 kW
Roller material GCr15 / Cr12MoV (heat-treated)
Roller shaft material: 40Cr
Cutter material: Cr12MoV (heat-treated)
Drive system: Motor-driven; gear and chain transmission
Cutting method: Hydraulic shearing
Electrical control: Fully automatic PLC control (Delta/Schneider)
Operators 1 person
Quality assurance: CE certified
IV. Production Process
Uncoiling & Feeding → Leveling → Servo Feeding/Punching → Guided Feeding → Roll Forming → Cut-to-Length → Collection Table
Process Step Description
Uncoiling & Feeding: Loads the steel coil onto the uncoiler to provide a continuous supply of material to the production line.
Leveling: Uses a multi-roller leveler for precision flattening; eliminates internal material stress to ensure accuracy in subsequent forming stages.
Servo Feeding & Punching: Employs a servo system for precise positioning; performs punching for mounting holes and other required hole patterns.
Guided Feeding: Automatically guides and aligns the material, ensuring smooth feeding for steel strips of varying widths.
Roll Forming: Uses a multi-pass, progressive cold-forming process to gradually shape the material into the required cross-section for the diagonal brace tie rod.
Cut-to-Length: Automatically cuts the material to the preset length using a hydraulic system; ensures high precision and clean, smooth cut edges.
Collection Table: Manual or automatic collection of finished products.
 English